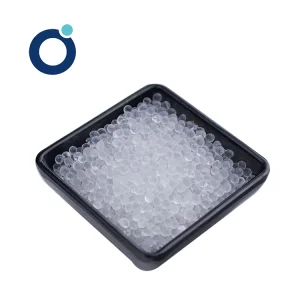
Engineered engineered materials delivering high kinetic absorption rates, minimal dust abrasion, and optimal pore diameter consistency.
A macroeconomic analysis of performance desiccants, gas dehydration, and environmental regulatory compliance.
In modern industrial processes, the demand for highly efficient purification and dehydration solutions is growing rapidly. Silica gel and molecular sieves are essential materials used in gas separation, petrochemical processing, moisture protection, and logistics. Industrial systems operate under high pressures, wide temperature fluctuations, and aggressive chemicals. Therefore, standard desiccant materials are no longer sufficient. Companies need highly engineered, synthetic silica gels and structurally stable alumina materials that offer long service cycles, reliable structural integrity, and low dust generation.
Internationally, dynamic growth across the pharmaceutical, semiconductor, and petrochemical fields drives the demand for specialized adsorbents. In regions like the EU and North America, strict environmental regulations require chemical processing plants to limit emissions and energy consumption. Achieving low dew points in compressed air systems directly lowers energy use by reducing the frequency of regeneration cycles. As a result, selecting an established factory that complies with global standards (such as ISO 9001:2008, REACH, and TUV guidelines) is a key strategic decision for global chemical supply chains.
Precise kinetic pore engineering (from 2Å up to 10Å) ensures selective molecular adsorption. This prevents co-adsorption of critical process chemicals and guarantees high product purity.
Advanced crystal engineering maintains structural integrity during high-temperature thermal regeneration cycles, extending the media's operational lifespan.
Our spheres are processed to achieve high crush strength. This prevents particle degradation and protects downstream equipment from dust contamination.
How specialized chemical media solves complex operational challenges in critical industrial sectors.
In high-pressure natural gas drying, gas streams must achieve dew points of -100°C (-148°F) to prevent hydrate formation before liquefaction. Our custom-formulated alumina silica gels and zeolites adsorb water vapor selectively while resisting degradation from heavy hydrocarbons and acid gases (like H2S and CO2). This protects critical liquefaction cold boxes and downstream machinery.
Cryogenic oxygen and nitrogen separation requires the complete removal of trace carbon dioxide and moisture before air liquefaction. This prevents blockages in cryogenic exchangers. Using our high-performance molecular sieves, such as the JZ-OI series, allows operators to optimize PSA and VPSA systems. This results in higher oxygen recovery rates, lower energy consumption, and longer cycle times.
For standard manufacturing plants and heavy factories, compressed air is a key utility. Moisture in these systems causes pipe corrosion, instrument failures, and quality defects. Utilizing standard-compliant activated alumina (manufactured under HG/T 3927-2007) and silica gel blends guarantees dry, clean compressed air, even in demanding and highly humid operating environments.
Moisture damage presents a constant challenge for global electronics logistics and pharmaceutical packaging. Utilizing specialized silica gel packs, such as our JZ-SG series, provides reliable relative humidity control within enclosed spaces. This safeguards active pharmaceutical ingredients and prevents micro-corrosion on delicate printed circuit boards.
A trusted global leader in chemical adsorption engineering, delivering premium desiccants and customized technical solutions since 1994.
Shanghai Jiuzhou Chemicals Co., Ltd. is located in Shanghai, China's largest economic development city. Over the years, Jiuzhou has adhered to the principles of "Quality Control & Innovation," committing itself to the research, development, and manufacturing of high-quality, innovative chemical products. Our key product lines include various molecular sieve powders, molecular sieves, activated powder, activated alumina, aluminum oxide catalysts, various types of alumina packing and ceramic balls, sodium silicates, aluminum hydroxide, zeolite 4A, sodium carbonates, and SLES, among others. All Jiuzhou products have passed the ISO9001:2008 quality management system certification, as well as TUV and SGS certifications, ensuring compliance with rigorous international safety and performance standards.
The Jiuzhou production facilities feature a world-class chemical research team and expert engineers. We utilize state-of-the-art international production technologies and advanced processing equipment. Our facilities are built in strict alignment with national environmental and safety standards. The central testing laboratory houses high-end analytical instruments to monitor and verify raw materials and finished goods, ensuring that every batch meets global industrial expectations.
Jiuzhou's technical expertise and industry reputation make it a leading name in the desiccant and chemical adsorption fields. With deep technical reserves, automated multi-functional production workshops, and specialized dynamic laboratories, we have developed a comprehensive operational system. Today, Joozeo products are exported worldwide, supported by distribution channels across the United States, Europe, Japan, Southeast Asia, North and South America, and the Middle East. We provide our global partners with reliable products, custom formulations, and energy-saving adsorption solutions.


We actively participate in formulating national and industrial chemical standards, demonstrating our commitment to quality leadership.

Adsorption compressed air dryers for general use

Activated aluminium oxide for industrial use

Refrigeration compressed air dryers for general use

Industrial compressed air system filtration standards

Adsorbent chemical application and safety guidelines

Green low-carbon manufacturing norms for adsorbents
Pioneering the next generation of energy-efficient, low-carbon industrial chemical materials.
The global chemical processing industry is moving toward carbon neutrality and higher energy efficiency. At Jiuzhou, our R&D efforts focus on developing adsorption materials that require lower regeneration temperatures, directly reducing energy usage in thermal swing adsorption (TSA) systems. By adjusting the surface chemistry of our silica gels and creating new composite materials (like alumina-silica gel hybrids), we aim to provide high moisture capacity along with excellent thermal stability.
Our long-term product roadmap focuses on three main engineering goals: first, increasing the mechanical crush strength of our beads to prevent system clogging and dust buildup; second, enhancing the selectivity of our molecular sieves to improve output in air separation plants; and third, implementing eco-friendly, zero-discharge manufacturing processes at our Shanghai and Wuxi production facilities. Through continuous innovation, Jiuzhou is committed to supplying high-performance, sustainable chemical solutions to partners around the world.

Better air, Better life. We design and manufacture our products to support global environmental protection, clean air, and sustainable industrial growth.








Expert insights on product selection, performance characteristics, and regeneration guidelines.
For blue and white silica gels, regeneration typically occurs between 120°C and 150°C. For industrial molecular sieves, regeneration is usually performed at temperatures ranging from 200°C to 320°C, depending on the fluid system and the specific adsorption cycle (such as TSA or PSA).
Regular silica gel can shatter or crack when it comes into direct contact with liquid water droplets, which reduces its mechanical strength. Water-resistant silica gel (such as JZ-WSAG) features a modified pore structure and surface chemistry. This allows it to absorb moisture from air stream liquids without breaking, protecting downstream equipment from dust.
Jiuzhou products comply with ISO 9001:2008 quality standards. Our manufacturing processes are verified by TUV and SGS certifications. Additionally, our industrial desiccants meet relevant national standard guidelines, including HG/T 3927-2007 (for activated alumina) and JB/T 10532-2017 (for adsorption dryers).
Custom-engineered porous media designed to maintain mechanical strength and adsorption efficiency in demanding process environments.
Connect with our technical support team to find the right chemical adsorption materials and solutions for your process design. We respond within 24 hours.
Send Request